[language-switcher]

China Top Stone Composite Floor Suppliers for Global Buyers

Global buyers are paying closer attention to Stone Composite Floor suppliers in China. The reason is practical. These products combine a mineral-filled core, decorative layers, and a protective wear surface. They can resemble limestone, oak, or terrazzo while supporting faster installation and easier maintenance.

Market research supports this growing interest. Grand View Research reports continued expansion in the global resilient flooring market, driven by residential renovation, commercial construction, and waterproof flooring demand. Fortune Business Insights also identifies luxury vinyl and rigid-core flooring as important growth segments, especially where durability and visual design matter. These reports do not measure every Stone Composite Floor shipment separately. That limitation matters.

China remains a major manufacturing base for rigid flooring, serving distributors, contractors, and private-label brands across Asia, Europe, North America, and the Middle East. Qualified suppliers commonly provide click-lock panels, embossed textures, low-VOC options, and thicknesses from approximately 4 to 8 millimeters. However, specifications vary widely. A 5-millimeter board is not automatically equal to another 5-millimeter board.

This guide examines China’s leading Stone Composite Floor suppliers through product quality, production experience, testing capacity, export documentation, and after-sales reliability. Evidence should include technical datasheets, wear-layer measurements, dimensional-stability results, and current compliance certificates. Samples also deserve attention. A floor may look convincing under showroom lights, yet reveal uneven joints after installation.

Details matter most. Choose carefully. Supplier claims require verification.
China Top Stone Composite Floor Suppliers for Global Buyers

Types of Stone Composite Flooring Offered by Chinese Suppliers

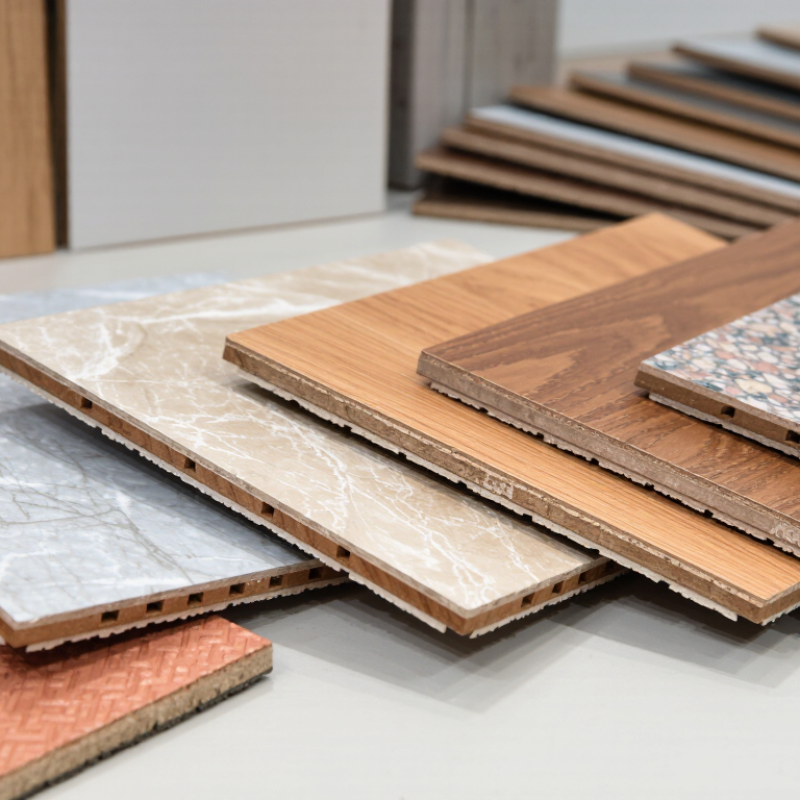
Chinese suppliers commonly produce stone composite flooring in several practical forms for global projects. The main category is SPC flooring, built with limestone powder, polymer resin, and stabilizers. Its dense core resists moisture and supports click installation over prepared subfloors. Many factories offer rigid planks, square tiles, and herringbone profiles. Surface films can imitate oak, slate, cement, or veined marble with sharp printed detail. Embossed textures add grip and reduce the flat appearance of basic printed floors.

Another option is glue-down stone composite tile, often supplied in thinner gauges. It suits retail refits, apartments, and rooms where doors limit floor height. Suppliers may also provide loose-lay formats for temporary displays or fast replacement areas. Some rigid products include acoustic underlays for apartments and hospitality spaces. Core density, wear-layer thickness, and locking accuracy deserve direct comparison. Ask for production samples, not only digital images. Small differences matter.

In technical reviews, buyers should check dimensional stability after heat exposure and moisture testing. A reliable supplier can share batch records, material declarations, installation guidance, and independent test reports. Fire, slip, and emissions data should match the destination market’s requirements. Do not judge quality by stone pattern alone. A beautiful sample can hide weak joints or uneven backing. Even reliable factories can show minor shade variation. That deserves attention. Request several cartons before approving a large order, because shade and locking performance may vary between batches.

Key Manufacturing Standards and Quality Control Practices

China’s top stone composite floor suppliers serve global buyers through controlled production and documented testing. Reliable factories inspect limestone powder, resin, stabilizers, and decorative films before mixing. They monitor formulation ratios because small deviations can affect hardness and dimensional stability.

Manufacturing should follow recognized testing methods, such as ASTM or EN procedures, where applicable. Quality teams commonly test wear resistance, slip performance, fire behavior, water absorption, and locking strength. They also measure plank thickness at several points, not only at the center. A temperature-controlled room helps confirm expansion and contraction results. Production records should connect each carton with a clear batch number.

Tips: Request recent test reports, inspection photos, and sample pieces from different batches. Check the carton labels, edge profiles, surface finish, and click-lock alignment. Ask how rejected planks are isolated and recorded.

Experienced buyers should inspect both laboratory results and real factory habits. During a pre-shipment inspection, verify color consistency under natural and indoor light. Check corners for chipping, since packing pressure can hide weak edges. Suppliers should use moisture-resistant packaging and stable pallet stacking. No factory is perfect. Even strong systems may miss a small surface mark. That is why random sampling, independent inspection, and corrective-action records matter. A supplier’s willingness to discuss defects often reveals more than polished certificates.

China Stone Composite Flooring Suppliers: Key Quality-Control Targets

Reference acceptance limits commonly included in global buyer specifications for stone composite flooring.

The chart highlights practical manufacturing checkpoints, including dimensional accuracy, thickness consistency, water absorption, and wear performance. Values are reference targets frequently used in supplier specifications; buyers should confirm the final limits against the applicable ASTM, EN, ISO, project, and installation requirements.

How to Evaluate Chinese Stone Composite Floor Manufacturers

China Top Stone Composite Floor Suppliers for Global Buyers

How to Evaluate Chinese Stone Composite Floor Manufacturers

Selecting a Chinese stone composite floor manufacturer requires more than comparing quotations. Factory experience matters. Ask how many years the company has produced stone composite flooring, not only traded it. Request production photos, equipment details, and recent export references. A serious manufacturer should explain its mixing, pressing, coating, and click-lock processes clearly. Visit the facility when possible. Check whether raw materials are labeled and stored above the floor.

Study the technical data carefully. Confirm the stone powder content, core density, wear-layer thickness, surface treatment, and dimensional tolerance. Request samples from different production batches. Place them in a room with changing temperature and humidity for several days. Check edge alignment, color consistency, surface scratches, and locking strength. Ask for test reports related to emissions, fire performance, slip resistance, and durability. Reports should identify the tested product, date, laboratory, and standard. Generic documents are weak evidence.

Supplier reliability also appears in small details. Can the team provide a clear packing plan, carton dimensions, loading photos, and realistic lead times? Ask how defects are recorded and handled after delivery. Independent pre-shipment inspection can reduce unpleasant surprises. A polished sample may hide uneven backing or fragile corners. That risk deserves attention. Do not rely on promises alone. Compare records, test results, communication speed, and the manufacturer's willingness to admit limitations. In some cases, the cheapest offer becomes expensive after replacement, delays, or installation waste.

China Top Stone Composite Floor Suppliers for Global Buyers - How to Evaluate Chinese Stone Composite Floor Manufacturers

Evaluation Dimension Weight What Global Buyers Should Review Typical Technical or Commercial Benchmark Recommended Verification Evidence
Product Construction 15% Confirm the floor structure, including the wear layer, printed decorative film, rigid stone-polymer core, balancing layer, and optional attached underlay. Common SPC constructions use a rigid mineral-polymer core. Total thickness is frequently about 4.0–6.5 mm, while attached underlay may add approximately 1.0–1.5 mm. Cross-sectional sample, technical data sheet, material declaration, and an independent thickness measurement.
Wear-Layer Performance 12% Assess resistance to abrasion and suitability for residential, commercial, or high-traffic applications. Wear layers commonly range from approximately 0.20–0.70 mm. Commercial projects generally require a higher wear-layer specification than light residential projects. Third-party abrasion report, product classification, sample testing, and written confirmation of the wear-layer thickness.
Dimensional Accuracy 10% Check plank length, width, thickness, squareness, straightness, click-joint fit, and locking consistency. Large variations can cause open joints, lippage, or installation difficulty. Buyers should set project-specific tolerances and require inspection records for each production batch. Caliper measurements, straightedge inspection, random carton sampling, and an approved pre-production sample.
Standards and Compliance 12% Verify that the product meets the legal and technical requirements of the destination market. Relevant references may include ISO 10582 for resilient floor coverings, EN 14041 for CE-related performance characteristics where applicable, and ASTM or local standards required by the importing country. Current test reports showing the exact product code, laboratory details, test method, issue date, and applicable market.
Indoor Air Quality 8% Review formaldehyde and volatile organic compound performance, especially for schools, healthcare facilities, and residential projects. Request formaldehyde test results using an applicable method such as EN 717-1 or the destination market’s recognized method. Low-emission claims must be supported by current reports. Emissions test report, raw-material declaration, laboratory accreditation details, and batch traceability.
Fire and Slip Performance 8% Match fire reaction and slip-resistance performance to the intended building type and local regulations. Performance varies by construction and surface treatment. Typical project requirements may include a documented fire classification and slip-resistance result such as an R-rating where applicable. Fire test report, slip-resistance report, installation instructions, and confirmation that results apply to the supplied surface finish.
Quality-Control System 10% Evaluate incoming-material inspection, in-process control, final inspection, defect classification, and corrective-action procedures. A reliable production system should record batch numbers, core formulation controls, dimensional checks, color consistency, locking performance, packaging checks, and nonconforming-product handling. Factory audit, inspection checklist, sample batch records, calibration certificates, and corrective-action examples with sensitive information removed.
Production Capacity and Consistency 8% Determine whether the supplier can maintain the required quality and delivery schedule during repeat orders. Capacity should be evaluated by confirmed production lines, operating shifts, product specifications, and available raw materials rather than by an unsupported annual-output claim. Factory visit or live video audit, production schedule, line list, capacity statement, and references for comparable order volumes.
Customization and Sampling 5% Review support for color matching, surface embossing, plank dimensions, packaging artwork, private-label documentation, and sample approval. Require an approved golden sample and written tolerance limits before mass production. Confirm whether custom tooling or cylinders involve additional charges and lead time. Signed sample approval, color standard, packaging proof, tooling quotation, and change-control procedure.
Packaging and Export Readiness 5% Check carton strength, pallet stability, moisture protection, labeling, loading method, and export documentation. Packaging should show product code, shade, batch number, coverage, quantity, installation information, and country-specific marks where required. Packaging specification, carton drop or compression test where relevant, loading photos, commercial invoice, packing list, and certificate documentation.
Commercial Terms and After-Sales Support 7% Compare quotation clarity, payment terms, warranty scope, replacement policy, claim response, and responsibility for confirmed defects. Warranty terms should define coverage period, exclusions, installation conditions, acceptable color variation, claim evidence, and resolution time. Do not rely on a warranty duration alone. Signed quotation, sales contract, warranty document, claim procedure, spare-stock policy, and written response-time commitment.
Buyer screening note: The percentages are a practical evaluation model rather than a supplier ranking. Final acceptance should be based on destination-market regulations, independent testing, approved samples, factory capability, and a controlled pre-shipment inspection.

Export Services, Certifications, and Global Shipping Capabilities

China’s stone composite floor suppliers support global buyers with structured export services. Experienced teams confirm specifications, colors, carton details, and loading plans before production. They usually provide commercial invoices, packing lists, bills of lading, and certificates of origin. Reliable suppliers also explain applicable standards instead of sending confusing document bundles. Certification may include ISO 9001, CE-related documents, or independent laboratory reports, depending on the destination market. Always verify document validity with the issuing organization.

Tips: Request a complete compliance file before placing a deposit. Check test dates, product names, and declared thicknesses carefully. A beautiful sample proves little. Ask for batch photos, pallet images, and a pre-shipment inspection. Small details often prevent expensive disputes.

Global shipping requires practical coordination. Suppliers should offer container loading plans, moisture-resistant packaging, corner protection, and clear carton markings. They may arrange port delivery, customs paperwork, and shipping under agreed Incoterms. Ask how they handle damaged cartons, delayed vessels, and missing documents. In real projects, delays sometimes come from unclear responsibilities rather than factory problems. I would also compare loading efficiency, not only unit price. One extra pallet can change the landed cost. Some suppliers communicate quickly but document poorly, so keep every revision in writing. That weakness deserves attention before a long-term order.

Steps for Selecting the Right Supplier for Your Market

Choosing a Chinese stone composite floor supplier requires more than comparing export prices. Your market decides the real checklist. Begin with local requirements for fire rating, slip resistance, emissions, and installation performance. Ask for current test reports from accredited laboratories, not scanned documents with unclear dates. Match the product structure to your climate, traffic level, and underfloor conditions. Rigid core floors may perform differently in humid coastal warehouses than in dry apartments. Request samples in several light shades and inspect edges, locking joints, backing, and surface texture. Small defects become expensive after container loading.

A practical supplier review should include a video call and, when possible, an independent factory audit. Check production lines, dust control, storage racks, quality records, and carton labeling. Ask how many inspectors check each batch and what happens when a panel fails. Reliable suppliers give clear answers and measurable corrective actions. Pricing is only one part. Compare minimum order quantities, payment terms, lead times, replacement policies, and packaging strength. Use a trial order before committing to a full container. Photograph cartons after a simulated warehouse move. That simple test can expose weak corners or poor pallet protection.

Communication deserves equal attention. Confirm drawings, color references, tolerances, and inspection points in writing. Time-zone delays can quietly damage a launch schedule. One overlooked detail can affect thousands of square meters. I once trusted a perfect sample and ignored inconsistent batch records. That was a costly lesson. Supplier selection is never completely certain. Keep a scorecard, review performance after every shipment, and leave room to change your decision.

Inquiry Form